A check valve can be simple in appearance but demanding to manufacture. A valve body may have only a few ports, a seat, internal passages, and mounting features, yet small dimensional or surface deviations can affect sealing, flow, assembly, and service reliability.
For OEMs and product developers, the problem is often not the basic valve design. The difficulty comes when the drawing reaches production. A critical bore may be machined from an unsuitable datum, a sealing surface may receive the wrong finish, or a thin valve body may move during clamping. Any of these issues can create problems during assembly or pressure testing.
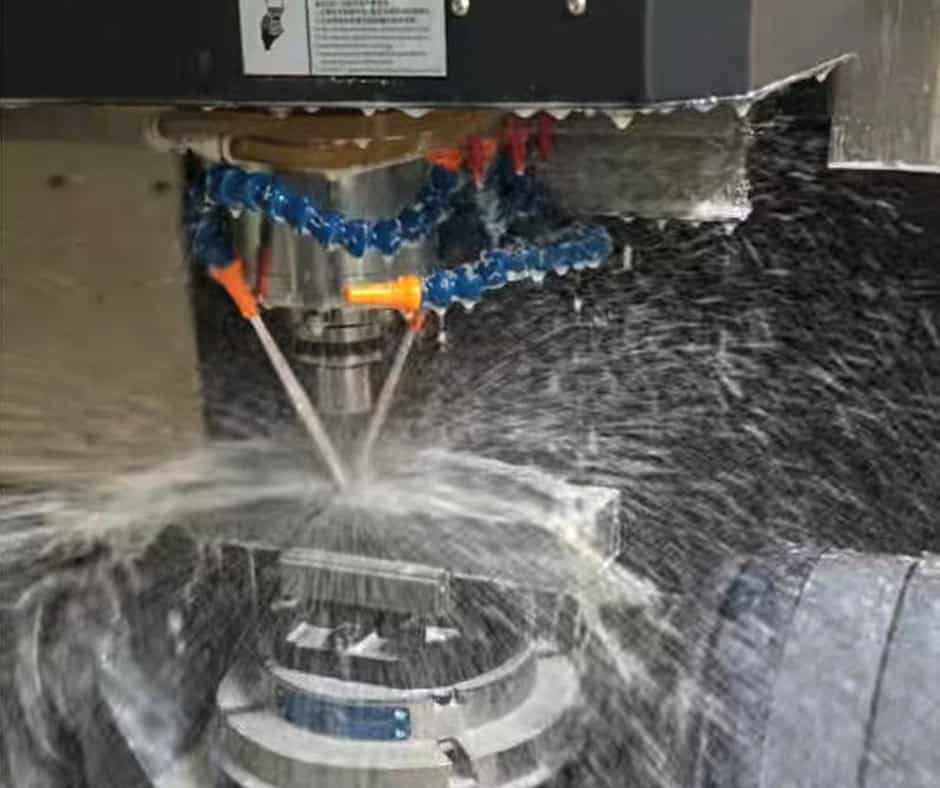
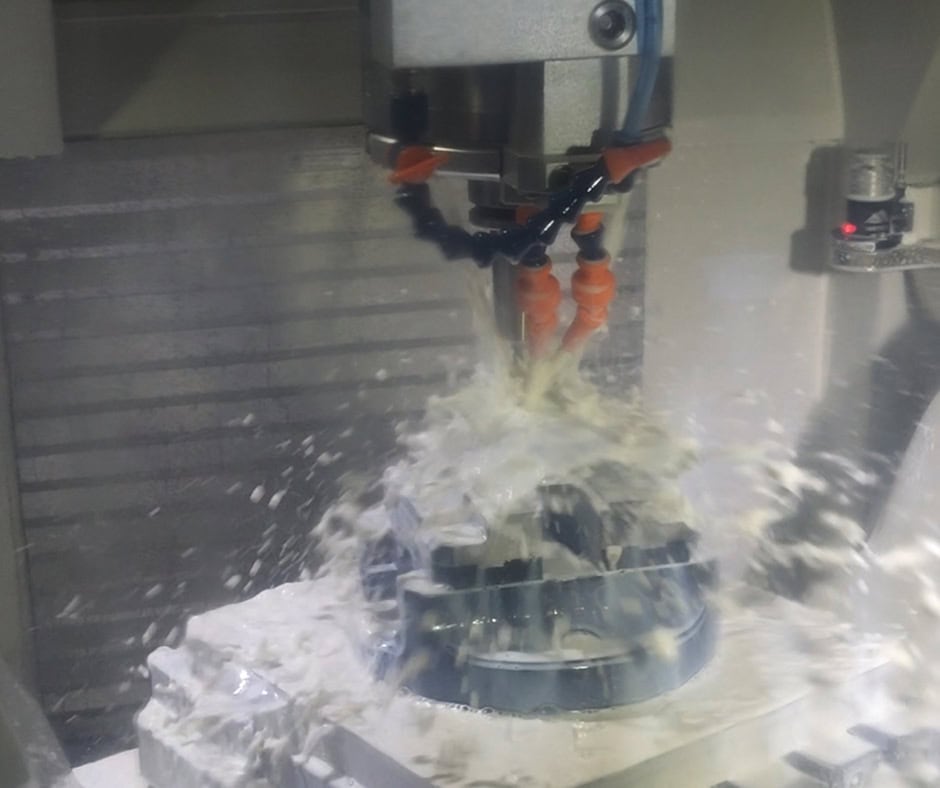
Check valve CNC machining provides a practical way to produce valve bodies, covers, seats, plugs, adapters, and other precision components, particularly when the design requires controlled dimensions, internal features, and repeatable production. However, the machining strategy needs to follow the functional requirements of the valve rather than simply reproducing the CAD model.
Table of Contents
1. Valve Body Accuracy Starts with the Right Datum
A common manufacturing problem occurs when several critical features are dimensionally correct on their own but are not correctly related to each other.
For example, the valve seat, internal bore, inlet port, outlet port, and mounting holes may all have individual tolerances. If these features are machined from inconsistent datums, their accumulated positional error can affect the relationship between the moving and stationary components.
Engineering principle
A datum establishes the reference from which other features are located or measured. For a check valve, the functional datum should normally be associated with the features that control assembly or fluid flow.
The relationship between the valve seat and internal bore can be more important than the absolute accuracy of a non-functional external surface. This is why geometric tolerances and datum references should be considered together rather than treating every dimension independently.
CNC manufacturing approach
A typical machining strategy is to establish a stable primary datum first, then use that reference for subsequent operations. Multi-axis CNC machining can reduce the number of setups when several features need to maintain positional relationships.
For valve bodies with intersecting ports, the machining sequence may include:
Face machining to establish a reference surface
Drilling or boring of the main passage
Precision machining of the valve seat area
Cross-hole or port machining
Thread machining
Mounting-hole machining
Final deburring and inspection
Reducing unnecessary repositioning can improve repeatability because every additional setup introduces another opportunity for alignment error.
Practical advice
When preparing drawings, identify which surfaces and bores actually control valve function. Use clear datums and specify position, concentricity, perpendicularity, or other geometric requirements only where they affect performance.
Avoid applying unnecessarily tight tolerances to every feature. Tight tolerances increase machining time and inspection requirements without necessarily improving valve performance.
2. Material Selection Has a Direct Effect on Machining and Valve Performance
The same check valve geometry can behave very differently depending on the material.
A valve used in general industrial equipment may have different material requirements from one exposed to corrosive fluids, elevated temperatures, or repeated mechanical loading. Material selection therefore needs to consider both the working environment and the manufacturing process.
Engineering principle
Common materials for machined valve components include stainless steels, carbon or alloy steels, aluminum alloys, brass, and engineering plastics.
Material affects:
Corrosion resistance
Mechanical strength
Wear resistance
Machinability
Surface finish
Dimensional stability during machining
Compatibility with the working fluid
For example, stainless steel can provide useful corrosion resistance but is generally more demanding to machine than aluminum or brass. Some grades can generate significant cutting heat or work hardening if machining parameters are poorly selected.
CNC manufacturing approach
The machining process should be adapted to the selected material rather than using the same cutting strategy for every valve body.
Aluminum valve components may allow higher cutting speeds and efficient material removal. Stainless steel may require better chip control, suitable tooling, and careful control of heat generation. Brass can provide good machinability for certain fittings and valve components, while engineering plastics require attention to deformation and thermal expansion.
Practical advice
Before production, specify the exact material grade rather than simply writing “stainless steel” or “aluminum.”
For OEM production, the drawing or purchase specification should clarify:
Material grade
Required mechanical properties where applicable
Corrosion requirements
Heat treatment, if required
Surface treatment
Material certification or traceability requirements
Material substitution should not be treated as a purely purchasing decision when the component contains sealing or pressure-related features.
3. Sealing Surfaces Require More Than Dimensional Accuracy
A valve can meet a dimensional inspection report and still fail to seal correctly.
This is particularly relevant to the seat, sealing face, internal bore, plug interface, and other surfaces that interact directly with the valve’s moving or sealing elements.
Engineering principle
A sealing interface depends on several factors at the same time:
Geometry
Flatness or roundness
Surface finish
Concentricity
Contact area
Material
Assembly relationship
Simply achieving a nominal diameter does not guarantee a functional sealing surface.
For cylindrical valve components, bore geometry and the relationship between mating diameters can influence how the components move and contact each other. For flat sealing interfaces, surface irregularities can create leakage paths even when the overall dimensions are within tolerance.
CNC manufacturing approach
Precision boring, turning, facing, and finishing operations can be selected according to the functional requirement.
Where a critical sealing surface is involved, it may be preferable to leave a controlled amount of material for a finishing operation rather than attempting to complete the feature in a single roughing pass.
The workholding method also matters. Excessive clamping force can distort thin-wall components. Once the component is released, the machined surface may move slightly relative to its clamped condition.
Deburring is another important step. Burrs around internal ports or intersecting passages can interfere with assembly, restrict flow, or become loose inside the valve.
Practical advice
Do not specify surface roughness only because a general machining standard suggests it. Identify the surfaces where finish has a functional purpose.
For critical sealing surfaces, communicate the required roughness and geometric tolerance directly on the drawing. If the sealing method is unusual, providing a section view or additional engineering note can prevent interpretation problems during manufacturing.
4. Workholding and DFM Can Determine Whether a Part Is Easy to Manufacture
Some check valve designs look straightforward in CAD but are difficult to machine efficiently.
Deep internal passages, thin walls, small cross holes, recessed sealing surfaces, and multiple intersecting features can all create manufacturing challenges.
Engineering principle
CNC machining requires the workpiece to be securely positioned while still providing tool access to the required features.
The ideal design is not necessarily the one with the fewest CAD features. It is the one that can be located, clamped, machined, inspected, and released without unnecessary complexity.
CNC manufacturing approach
For a valve body with several ports, the machinist may need to consider the sequence of operations before production begins.
A practical DFM review should examine:
Tool access to internal and external features
Minimum internal corner radii
Hole depth relative to diameter
Thread accessibility
Wall thickness
Clamping surfaces
Number of required setups
Chip evacuation
Deburring access
If the component requires several orientations, fixtures or soft jaws may be developed to provide repeatable positioning.
For low-volume production, standard workholding may be more economical than a dedicated fixture. For recurring production, a dedicated fixture can reduce setup time and improve repeatability.
Practical advice
Ask the machining supplier to review the CAD model before releasing the design for production.
A small design change—such as adding a suitable clamping surface, increasing a difficult internal radius, or modifying a deep pocket—can sometimes have a greater effect on manufacturing cost than simply negotiating the machining price.
5. Inspection Should Focus on Functional Features, Not Just a Final Dimension Check
Inspection is particularly important when a check valve contains several features whose relationships affect assembly and performance.
A final dimensional check alone may not identify every manufacturing issue.
Engineering principle
Inspection should reflect the risk associated with each feature.
For example, an external mounting surface may have a relatively low functional risk, while the bore that guides a valve component may require much tighter control.
Depending on the design, inspection may involve:
Calipers and micrometers
Bore gauges
Height gauges
Thread gauges
Pin gauges
CMM inspection
Surface roughness measurement
Visual inspection
Functional or pressure testing where specified
CMM inspection can be useful when multiple features must be verified relative to common datums rather than simply measured as isolated dimensions.
CNC manufacturing approach
Critical dimensions should ideally be checked during production rather than waiting until the entire batch is complete. In-process inspection can identify tool wear, dimensional drift, or setup problems earlier.
For repeat orders, inspection data can also help identify process trends. If a critical bore gradually moves toward its tolerance limit, corrective action can be taken before nonconforming parts accumulate.
Practical advice
Separate critical-to-function dimensions from general dimensions in the drawing and inspection plan.
If pressure testing, leak testing, or other functional testing is required, define the test method and acceptance criteria before production. Dimensional inspection and functional testing answer different questions: one verifies geometry, while the other verifies whether the assembled component performs as required.
6. Material and Manufacturing Process Comparison
The appropriate manufacturing approach depends on the valve design, material, quantity, and required tolerances.
| Option | Typical Strength | Manufacturing Considerations | Suitable Use |
| Aluminum CNC machining | Lightweight and highly machinable | Relatively efficient material removal; consider deformation on thin sections | Lightweight valve bodies, equipment components |
| Stainless steel CNC machining | Corrosion resistance and strength | More demanding cutting conditions and tool control | Industrial and fluid-handling components |
| Brass CNC machining | Good machinability and corrosion resistance in suitable environments | Efficient for many turned components and fittings | Valve fittings, adapters, smaller components |
| Steel CNC machining | High strength and wear resistance | May require heat treatment or additional finishing | Mechanically loaded components |
| Engineering plastic machining | Low weight and chemical resistance for selected applications | Thermal expansion and clamping deformation require attention | Non-metallic components and selected fluid applications |
| CNC machining + secondary finishing | Flexible geometry with controlled final surfaces | Adds processing steps and cost | Components with critical surface or dimensional requirements |
The material should ultimately be selected according to the valve’s operating environment and functional requirements rather than machining convenience alone.
7. Prototype and Low-Volume Check Valve Production
For new valve designs, the first production stage often involves prototypes or relatively small quantities.
This is where CNC machining can be useful because the process does not require a dedicated mold or large tooling investment for each new geometry. Engineers can manufacture valve bodies or related components directly from CAD data, evaluate fit and function, and make design changes before committing to larger production volumes.
However, CNC machining does not automatically make every prototype inexpensive. Complex internal geometries, difficult materials, multiple setups, and tight tolerances can still increase cost significantly.
For prototype work, it is usually more efficient to identify the truly critical features and avoid unnecessary cosmetic or dimensional requirements.
When the design moves into repeated production, the manufacturing process can then be optimized around:
Fixture repeatability
Tool life
Cycle time
Setup reduction
Batch size
Inspection frequency
Material utilization
This transition from prototype machining to stable production should be considered during DFM review rather than after production problems occur.
8. Practical Considerations Before Ordering CNC Check Valve Components
Before sending a check valve component to a CNC machining supplier, OEMs and procurement teams should confirm the following:
1.Complete drawing – Include dimensions, GD&T, datums, threads, and critical features.
2.3D CAD file – STEP or another suitable neutral format can help the manufacturer review geometry and tool access.
3.Exact material grade – Avoid broad descriptions such as “stainless steel” when a specific grade is required.
4.Critical tolerances – Clearly identify dimensions that affect sealing, movement, alignment, or assembly.
5.Surface finish requirements – Specify roughness where it has a functional purpose.
6.Quantity and production stage – Prototype, low-volume batch, or recurring production can require different manufacturing strategies.
7.Inspection requirements – Define whether dimensional reports, CMM reports, material documentation, or functional testing are required.
It is also useful to clarify whether the supplier is expected to perform deburring, cleaning, surface treatment, marking, packaging, or other secondary operations.
9. Conclusion
The main manufacturing challenge in a check valve is rarely producing the basic shape. The more important issue is controlling the relationship between functional features.
Valve seats, internal bores, ports, threads, mounting surfaces, and sealing interfaces need to work together. Datum selection, workholding, material behavior, surface finish, machining sequence, and inspection therefore have a direct effect on the final component.
A well-planned check valve CNC machining process can provide the flexibility needed for prototypes and low-volume production while maintaining control over critical geometry. The key is to start with the functional requirements, translate them into practical tolerances and datums, and then design the machining and inspection process around those requirements.
For OEMs and procurement teams, early DFM communication is often more valuable than simply comparing machining prices. A manufacturable design, clearly defined critical features, and an appropriate inspection plan can reduce rework, simplify assembly, and make production more predictable.
10. FAQ
What materials are commonly used for CNC machined check valve components?
Common choices include aluminum alloys, stainless steels, carbon or alloy steels, brass, and selected engineering plastics. The correct material depends on pressure, temperature, fluid compatibility, corrosion exposure, wear, and mechanical requirements.
How important is surface finish for CNC machined valve components?
It depends on the feature. Surface finish can be particularly important on sealing and sliding interfaces, while many external non-functional surfaces do not require the same level of finish. The drawing should identify functional surface requirements rather than applying one finish specification to the entire component.
Can CNC machining be used for prototype and low-volume check valve production?
Yes. CNC machining is particularly suitable when valve components require relatively complex geometry, precision features, or frequent design changes. For larger recurring volumes, fixture design, tool selection, cycle-time optimization, and alternative manufacturing processes may become important when evaluating total production cost.